

RoxxAsphalt is our own asphalt plant control system. It gives operators and plant managers all the functions of modern controls – without replacing the entire automation at once.
Upgrade without replacing everything
On many plants, e.g. Ammann, a new control system usually means replacing all communication modules at once. RoxxAsphalt communicates with old and new communication modules at the same time. You replace old modules gradually as they wear out – spreading the cost over time.
Implementation within one month
We have proven that we can go from order to commissioning within one month. We plan the changeover to keep plant downtime to a minimum.
The whole plant on one screen
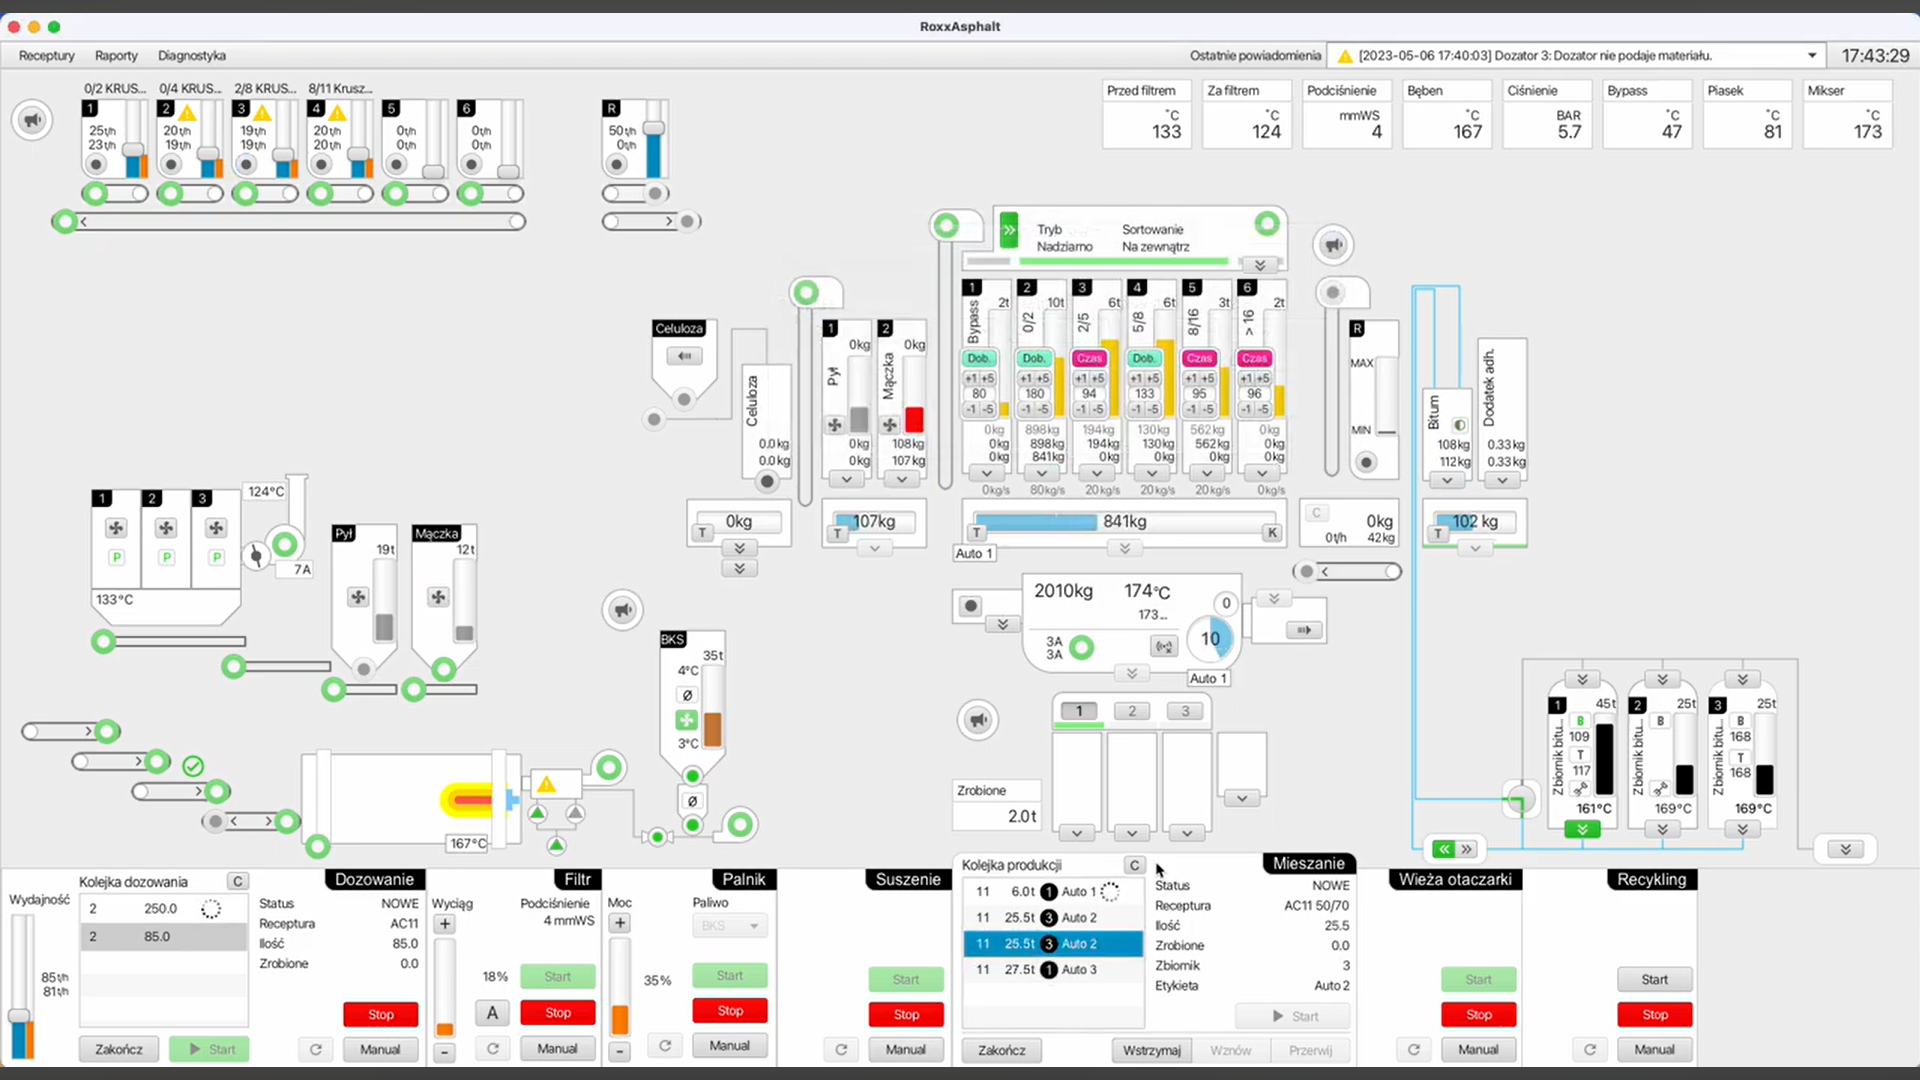
A clear main screen shows the entire process – from cold feed, through drying and the tower, to the mixer, loading silos and bitumen tanks. Each area has its own Start/Stop control and automatic and manual modes.
Operator functions
- Cold feed – set and actual output of each feeder (t/h), feed queue, RAP feeder.
- Drying, burner and filter – burner output, fuel selection, exhaust fan and negative pressure control, temperatures before and after the filter, drum and bypass.
- Tower and weighing – hot bins with weighing tolerances, sorting and oversize mode, weighing of aggregates, filler, cellulose, bitumen and adhesion agent.
- Mixer – batch size, mix temperature and mixing time in real time.
- Production queue – orders with recipe, quantity and target silo, processed automatically one after another; produced tonnage counter.
- Bitumen tanks and silos – levels and temperatures in real time.
- Recycling – control of the RAP feed line.
- Notifications – with date and time, e.g. when a feeder is not delivering material, with a warning shown at the equipment.
Precision and automation
- Accurate weighing – coarse and fine dosing, dynamic correction during weighing and automatic tare correction.
- Bitumen correction – bitumen quantity calculated from the actual aggregate weight and deviations of the previous batch.
- Cold feed control – feeder output matched to tower demand and hot bin levels.
- Burner and negative pressure control – automatic control of aggregate temperature at the drum outlet while monitoring exhaust gas temperature and negative pressure.
- Start/stop sequences – automatic start-up and shutdown of equipment groups in the right order with defined delays.
- Parameter protection – settings for scales, mixer, burner and feeders are password-protected.
Plant manager functions
- Recipes – creating and managing mix recipes, order queue.
- Reports and archive – every batch recorded, archive search by date and order, printing and export of reports.
- Statistics – produced quantities, aggregate and bitumen consumption, deviation and temperature trends – daily, monthly and long-term.
- Diagnostics – message history with tracing to the source of the fault and a view of module inputs and outputs.
- Integration – transfer of production data to higher-level systems over the network.
Benefits
- Lower upgrade costs – modules replaced in stages.
- Short implementation time.
- Support and development directly from the manufacturer – ROXX TECH.
Want to upgrade your controls? Contact us.